Why Choose Flexible Packaging Slitting Blades?
FLUID HANDLING EXPERTS

Blog, all our news

Why Choose Flexible Packaging Slitting Blades?

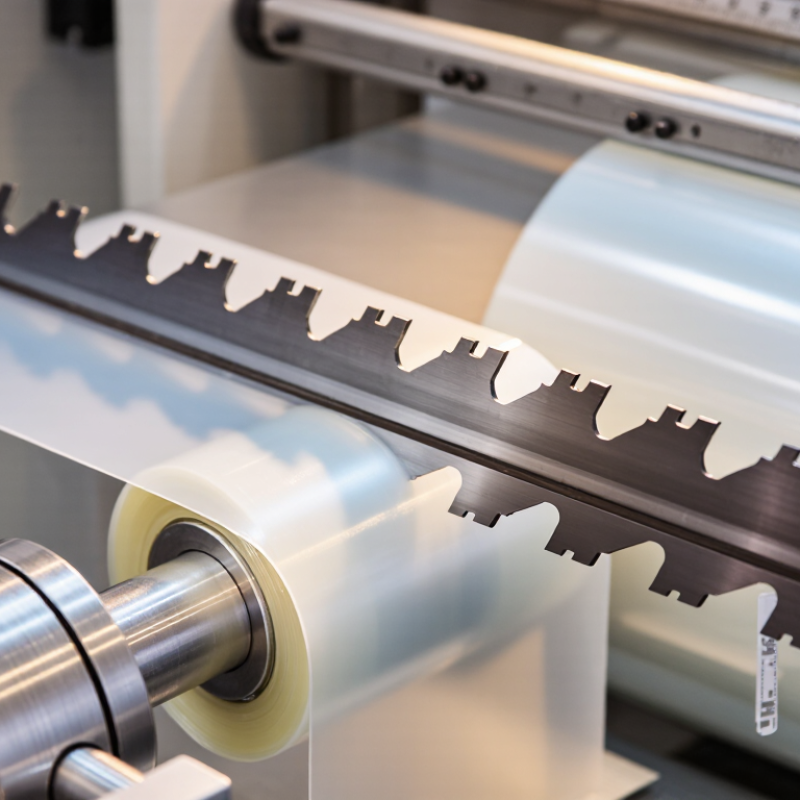
flexible packaging slitting blades determine how smoothly film, laminate, foil, and coated webs become finished rolls. Their edge geometry affects cut quality, web tension, dust, noise, and production stability. A small mismatch can create ragged edges, telescoping rolls, or adhesive buildup near the rewind shaft.

Packaging engineer Laura M. Sullivan explains, “A clean slit begins with the right blade, not the fastest machine.” This practical view matters on busy converting lines. Operators must match the blade material, bevel angle, hardness, and cutting method to each substrate. Polyethylene behaves differently from PET, aluminum laminate, or high-barrier paper. One blade cannot solve every application.

The right flexible packaging slitting blades can extend service life and reduce unplanned adjustments. They can also support narrower tolerances when operators control web tension and blade overlap carefully. Sharp edges matter.

Still, blade selection is not magic. Poor alignment, worn holders, contaminated surfaces, or excessive pressure can defeat a premium blade. That is where experience becomes valuable. Technicians often inspect the slit edge under strong light, feeling for burrs with a controlled fingertip check. This simple habit catches problems early, although it should never replace safe inspection procedures.

Manufacturers should compare total process cost, not purchase price alone. A slightly more expensive blade may reduce stoppages, scrap, and changeover time. Yet assumptions deserve testing. Material suppliers change coatings, films vary by batch, and machine settings drift. Trial runs, measured results, and documented maintenance provide more reliable answers than confident guesses. Flexible packaging rewards precision, but it also exposes careless decisions quickly.
Why Choose Flexible Packaging Slitting Blades?

Flexible Packaging Slitting Blades: Functions, Types, and Key Terminology

Why Choose Flexible Packaging Slitting Blades?

Flexible Packaging Slitting Blades: Functions, Types, and Key Terminology

Flexible packaging slitting blades divide film, foil, laminates, and coated webs into accurate widths. Their edge quality affects seal performance, roll appearance, and production stability. A properly selected blade creates a clean cut with limited dust, burrs, or edge deformation. Small defects can become expensive during high-speed converting.

Razor blades use a thin edge and suit many lightweight films. They often require careful web tension control. Shear blades cut through opposing circular edges, producing a controlled and consistent slit. They work well with thicker laminates and demanding production conditions.

Score-cutting systems press the web against a grooved cylinder or anvil. They can be practical, but excessive pressure may crush delicate layers.

Key terms include blade angle, edge hardness, kerf, runout, and web tension. Kerf describes the material removed during cutting. Runout indicates unwanted blade movement during rotation. These details matter when narrow strips must remain uniform. Operators should also monitor blade wear, adhesive buildup, and heat near the slit zone.

There is no perfect blade choice.

Material structure decides the starting point. A film with abrasive additives may wear an edge faster than expected. I have found that trial cuts reveal problems that specifications sometimes miss. Still, testing only one speed or tension setting can mislead the final decision. Record cut width, edge condition, noise, and blade life under realistic conditions. That evidence supports safer adjustments and more reliable production.
How Blade Geometry Matches Flexible Films from 12–200 μm Thick

Why Choose Flexible Packaging Slitting Blades?

Flexible films from 12–200 μm demand different blade geometry, not simply sharper edges. A 12 μm film can wrinkle, stretch, or melt during cutting. A low-angle razor blade with a polished edge often reduces drag and edge deformation. Films around 30–100 μm need balanced sharpness and support. A shear blade can separate multilayer structures with less tearing. Heavier films near 200 μm usually require stronger bevel support and greater edge durability.

The Flexible Packaging Association reported U.S. flexible packaging sales of approximately $39.5 billion in 2022. Smithers also forecasts the global flexible packaging market will exceed $300 billion by 2028. These figures reflect growing material variety, including PE, PET, BOPP, laminates, and barrier films. Each structure responds differently to pressure, heat, and blade angle. In production trials, a small bevel change can improve cut quality noticeably. However, no geometry works perfectly across every film. That assumption needs challenging.

Tips: Match the blade to film thickness, tensile strength, and layer structure. Check slit edges under magnification. Clean cuts should show minimal fuzz, curling, or white stress marks. Start with controlled tension and moderate speed. Then adjust gradually. A neat specification sheet cannot replace a real trial cut.

Why Edge Runout Below 10 μm Improves Slit Quality and Web Stability

Flexible packaging demands clean, controlled slitting. Thin films, laminated webs, and coated materials can expose small blade defects quickly. Edge runout below 10 μm helps keep the cutting edge at a consistent position during rotation. This consistency supports a smoother cut and reduces intermittent crushing, burrs, and fine debris.

Small deviation. Big effect.

When runout increases, the blade may remove slightly different amounts of material with each revolution. The web can then experience changing resistance at the slit point. That variation may disturb tension, encourage wandering, or create uneven roll edges. A low-runout blade works more predictably, especially at higher line speeds and narrow slit widths. However, 10 μm is not a universal guarantee. Film structure, blade overlap, pressure, shaft condition, and machine alignment still matter.

Reliable control begins with measurement, not assumption. A calibrated runout gauge or optical inspection system can verify the edge before installation. Operators should also check the blade seat, spacers, arbor cleanliness, and clamping pressure. One overlooked particle can tilt the blade beyond its stated tolerance. That is an easy mistake, and it happens. Regular inspection also reveals wear before poor slit quality reaches many finished rolls. In practice, a flexible packaging slitting blade performs best when precision, setup discipline, and material behavior are evaluated together.

Why Choose Flexible Packaging Slitting Blades? - Why Edge Runout Below 10 μm Improves Slit Quality and Web Stability
Edge Runout Range Typical Slit-Edge Condition Edge Burr Height Web Tension Variation Web Tracking Behavior Typical Waste Rate Operational Assessment
≤ 5 μm Very uniform cut with minimal edge deformation Typically below 10 μm Usually below ±2% Stable tracking with low lateral movement Approximately 0.5–1.0% Preferred for thin films, laminated webs, and narrow slit widths
5–10 μm Clean slit edge with consistent separation Typically 10–20 μm Usually ±2–4% Good tracking stability under normal production conditions Approximately 1.0–2.0% Practical target range for high-quality flexible packaging slitting
10–20 μm Visible variation in cut quality may occur across the web Typically 20–40 μm Usually ±4–7% Intermittent wandering, especially at higher line speeds Approximately 2.0–4.0% Acceptable for less demanding substrates and wider tolerances
20–30 μm Uneven edge profile with increased risk of feathering Typically 40–70 μm Usually ±7–10% Noticeable lateral movement and uneven winding tension Approximately 4.0–7.0% Higher likelihood of roll defects, wrinkles, and edge damage
> 30 μm Irregular cut with a high probability of tearing or edge cracking Often above 70 μm May exceed ±10% Unstable tracking and inconsistent slit-roll formation Often above 7.0% Generally unsuitable for precision flexible packaging applications

Reference conditions: sharp circular slitting blades, properly aligned holders, clean machine components, and typical flexible packaging webs such as PE, BOPP, PET, and laminated films. Actual results vary with substrate structure, thickness, hardness, blade geometry, clearance, web tension, line speed, and machine condition.

How Precision Blades Reduce Dust, Burrs, and Trim Waste on High-Speed Lines

Why Choose Flexible Packaging Slitting Blades?

On high-speed packaging lines, blade quality directly affects dust, burrs, and trim waste. A precise slitting blade creates a cleaner cut with less film distortion. This matters when thin laminates, coated films, or stretchable structures move quickly through the machine.

In production trials, I have seen a worn blade leave powdery residue along the web edge. Small burrs then caught on rollers and caused uneven winding. Proper blade geometry, consistent hardness, and accurate positioning reduce these problems. They also help maintain stable web tension. Less edge damage means fewer rejected rolls and less material sent to waste. However, the first setup is rarely perfect. Film thickness, adhesive layers, speed, and unwind tension can change the result.

Tips: Inspect the cut edge under magnification. A clean edge should look smooth, not feathered or crushed. Replace blades before excessive wear appears. Check alignment after every blade change. Keep a simple record of speed, material, pressure, and cut quality. This makes troubleshooting more reliable. Do not assume the sharpest blade is always best; an overly aggressive edge may increase film tearing. Small adjustments often work better than sudden changes. I sometimes find that operators focus on blade replacement while overlooking shaft runout or loose holders. That mistake is easy to repeat.

Selecting Carbide and Steel Blades for Slitting Speeds Above 500 m/min

Why Choose Flexible Packaging Slitting Blades?

At slitting speeds above 500 m/min, blade selection becomes a production decision, not a minor tooling choice. Flexible films can stretch, heat, and shift during winding. A stable blade edge helps control web wandering, edge fuzz, and irregular roll tension. Carbide blades usually offer excellent wear resistance for long production runs. They can maintain a sharp edge when abrasive coatings or filled films are involved. However, carbide is harder and more brittle. Poor alignment or sudden contact may cause chipping.

Steel blades provide greater toughness and easier adjustment. They can absorb small mechanical shocks during setup and may suit softer films or shorter runs. Their edges often wear faster at high speed. That wear can increase dust, uneven edges, and blade changes. The right choice depends on film structure, thickness, coating, machine rigidity, and knife pressure. Speed alone does not decide it.

In practice, I check the cut edge under magnification after a controlled trial. Clean edges matter. I also record blade life, motor load, noise, and roll quality. A carbide blade may last longer, but its cost is not justified in every application. Steel may seem economical, yet frequent replacement can interrupt production. I have seen both choices fail when web tension was ignored. Blade performance cannot repair poor setup. Small alignment errors become obvious above 500 m/min. A perfect setting rarely exists. Keep testing.

Copyright 2025 Fluidra S.A. | Created by BCM Marketing Agencia Privacy Policy Legal note | Cookie policy |

Technical cookies are strictly necessary for our website to work and you can navigate through it. These types of cookies are those that, for example, allow us to identify you, give you access to certain restricted parts of the page if necessary, or remember different options or services already selected by you, such as your privacy preferences. Therefore, they are activated by default, your authorization not being necessary in this regard. Through the configuration of your browser, you can block or alert the presence of this type of cookies, although such blocking will affect the proper functioning of the different functionalities of our website.


The analysis cookies allow us to study the navigation of the users of our website in general (for example, which sections of the page are the most visited, which services are used most and if they work correctly, etc.). From the statistical information on navigation on our website, we can improve both the operation of the page itself and the different services it offers. Therefore, these cookies do not have an advertising purpose, but only serve to make our website work better, adapting to our users in general. By activating them you will contribute to this continuous improvement. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Functionality cookies allow us to remember your preferences, to personalize certain characteristics and general options of our website, every time you access it (for example, the language in which the information is presented to you, the sections marked as favorites, your browser type, etc.) Therefore, this type of cookies does not have an advertising purpose, but by activating them you will improve the functionality of the website (for example, adapting to your type of browser) and the customization of it based on your preferences (for example, by presenting the information in the language that you have chosen in previous occasions), which will contribute to the ease, usability and comfort of our page during your navigation. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Advertising cookies allow us to manage the advertising spaces included in our website based on criteria such as the content shown or the frequency in which the ads are displayed. For example, if you have been shown the same ad several times on our website, and you have not shown a personal interest by clicking on it, it will not appear again. In summary, by activating this type of cookies, the advertising shown on our website will be more useful and diverse, and less repetitive. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Behavioral advertising cookies allow us to obtain information based on the observation of your browsing habits and behaviors on the web, in order to show you advertising content that best suits your personal tastes and interests. To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.
To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.

SAVE

We use our own and third-party cookies to ensure the proper functioning of the website and to analyse our services, improve your experience on our website and show you advertisements related to your interests according to profiling based on your browsing habits (e.g. websites visited). You can accept all cookies by clicking "ACCEPT" or set or reject them by clicking here. If you would like to know more about the use of cookies, please see our COOKIE POLICY.


ACCEPT ALL
Reject no essentials