Top Metal Surface Finishing Methods for 2026
FLUID HANDLING EXPERTS

Blog, all our news

Top Metal Surface Finishing Methods for 2026

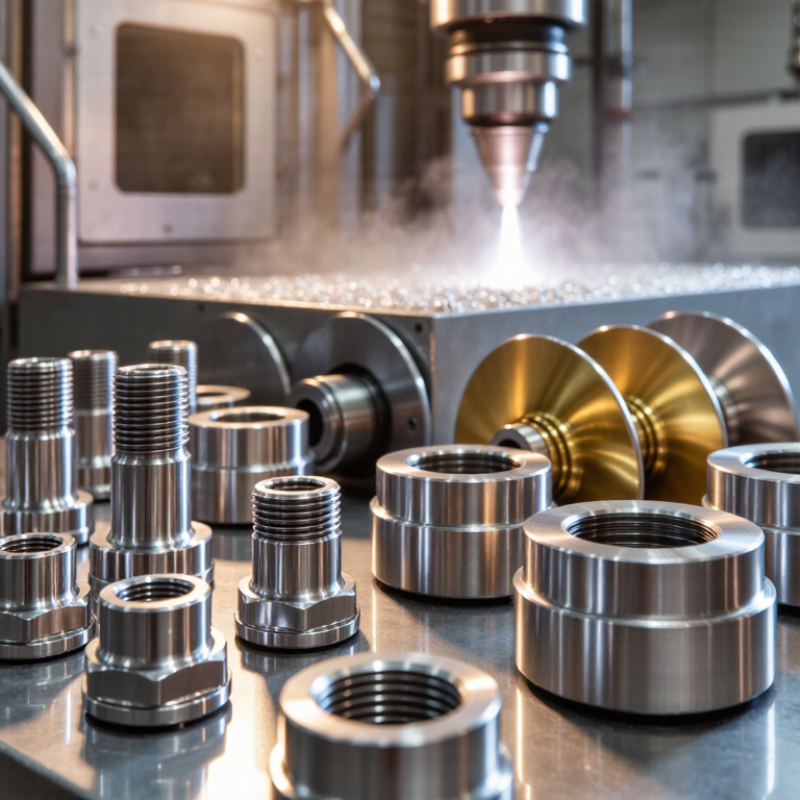
Metal Surface Finishing is more than a final coat of shine. It controls corrosion, wear, electrical contact, and appearance across parts as different as fasteners, medical instruments, and turbine components. In 2026, manufacturers will weigh familiar processes such as electroplating and anodizing against physical vapor deposition, thermal spraying, electropolishing, and conversion coatings. The right choice depends on the substrate, service environment, required thickness, and production volume. A polished sample alone cannot answer every question.

Grand View Research estimated the global metal finishing market at USD 104.7 billion in 2023 and projected a 4.7% compound annual growth rate through 2030. This is a market forecast, not a guarantee for any one process or factory. Still, it signals sustained demand for durable, precisely finished components. Corrosion engineer Pierre R. Roberge writes, “Corrosion is the destructive attack of a material by reaction with its environment.” That warning helps explain why coating selection must begin with how a part will actually be used.

In practice, details matter: a thin coating on a threaded bolt can affect fit, while a poorly prepared surface can undermine adhesion. This guide compares leading methods by performance, cost considerations, finish quality, and suitable applications. It also considers process control and environmental trade-offs, which vary by chemistry and facility. No method wins everywhere. Some comparisons remain imperfect, because suppliers and operating conditions differ; readers should verify specifications with qualified finishers before committing to production.
Top Metal Surface Finishing Methods for 2026

Prepare Steel to ISO 8501-1 Sa 2½ Before Applying a Finish

Top Metal Surface Finishing Methods for 2026

Before choosing a coating or other finish, prepare steel to ISO 8501-1 Sa 2½. This grade calls for very thorough blast cleaning. Visible oil, grease, dirt, mill scale, rust, and old coatings should be removed. Any remaining traces should appear only as slight stains, spots, or stripes. Look closely at weld toes, bolt holes, and the shadow beneath brackets. These spots can hold rust or dust. Easy to miss. Sa 2½ describes visual cleanliness, not every factor that affects coating life. Check surface profile, dust, soluble salts, and climate against the finish specification. A clean-looking panel can still fail.

AMPP’s 2016 IMPACT study estimated annual corrosion costs at US$2.5 trillion, about 3.4% of global GDP. It also estimated that improved corrosion management could save 15–35%. Those are global estimates, not a promise for any individual asset. On site, compare the prepared steel with ISO 8501-1 reference images under good lighting. Record the inspection and the time between blasting and coating. If flash rust appears, reassess before applying the finish. I would not treat a photograph as proof alone; dust and salts need separate checks. The process is not always tidy, and neither is real steel.

Top Metal Surface Finishing Methods for 2026 — Prepare Steel to ISO 8501-1 Sa 2½ Before Applying a Finish

Surface Preparation Method How It Works ISO 8501-1 Classification Suitability for Sa 2½ Key Considerations Before Finishing
Compressed-air abrasive blasting Compressed air propels abrasive media against the steel to remove rust, mill scale and old coatings. Sa grades apply to blast-cleaned steel. Suitable. The process can achieve Sa 2½ when the specified visual cleanliness is met. Remove oil, grease and dirt before blasting. Select an abrasive and blasting procedure that produce the profile required by the coating specification.
Centrifugal wheel abrasive blasting Rotating wheels propel abrasive onto steel, commonly in production lines or automated blast-cleaning equipment. Sa grades apply to blast-cleaned steel. Suitable. Sa 2½ can be achieved when the cleaned surface meets the standard’s visual requirements. Check coverage, equipment settings and the condition of the abrasive. Confirm the result on the actual workpiece, including edges and less-accessible areas.
Power-tool cleaning Powered wire brushes, grinders or needle scalers remove loose rust, paint and other surface material. St grades: St 2 and St 3. Not a Sa 2½ method. Power-tool cleaning is classified separately from abrasive blast cleaning. Useful for localized preparation or maintenance where blasting is impractical. Follow the coating specification for the required preparation grade and surface condition.
Hand-tool cleaning Manual scraping, wire brushing or abrading removes loose surface contamination and corrosion products. St grades: St 2 and St 3. Not a Sa 2½ method. Generally suited to small areas or limited repairs. It does not provide the same blast-cleaned condition or profile control as abrasive blasting.
High-pressure water jetting Pressurized water removes contaminants and corrosion products; abrasive may be added in some processes. Water-jetting preparation is addressed separately in ISO 8501-4, using Wa designations. Not designated Sa 2½. Water-jetting grades should not be reported as Sa grades. Assess the surface under the applicable water-jetting criteria. Consider residual salts, drying and possible flash rust before applying a coating.
Chemical pickling Acid-based treatment removes rust and mill scale through chemical reaction, followed by rinsing and drying. Does not receive an Sa 2½ designation under ISO 8501-1. Not a Sa 2½ method. Control chemical concentration, rinsing and residue removal. Verify that the resulting surface condition meets the finish supplier’s requirements.
Laser cleaning A controlled laser beam removes or reduces surface contaminants and coatings. No Sa 2½ designation under ISO 8501-1. Not automatically equivalent to Sa 2½. Validate the process for the specific steel, contamination and finish. Confirm cleanliness and any required surface profile using the applicable project criteria.

Practical check: ISO 8501-1 Sa 2½ means very thorough blast-cleaning: when viewed without magnification, the surface is free from visible oil, grease and dirt, and from most mill scale, rust, coatings and foreign matter; any remaining traces are limited to slight staining in the form of spots or stripes. Specify the required surface profile separately and verify it before coating.

Compare Blasting, Grinding, and Polishing by Surface-Roughness Targets

For a target near Ra 3.2 μm, grinding can remove tool marks without adding a deep anchor pattern. Finer grinding may reach roughly Ra 0.8 μm, while polishing can take parts below Ra 0.4 μm. These are planning ranges, not guarantees; alloy, abrasive sequence, and measurement direction all matter. ISO 21920-2:2021 defines profile parameters such as Ra, helping teams specify and verify texture consistently.

Blasting is useful when coatings need a mechanical key, but its profile should not be mistaken for Ra. ISO 8503-1:2012 lists nominal comparator values of 25, 60, and 100 μm for fine, medium, and coarse blast profiles. Those values describe comparator grades, not Ra readings. The process ladder is imperfect: blasting may improve coating adhesion while missing a tight Ra limit, and polishing can round a crisp edge.

Tips: Put the required Ra, cutoff, and measurement direction on the drawing. Check a representative area after each process change. A glossy surface can still be rough; verify it with a calibrated profilometer, not visual inspection alone.

Use Electroplating or Electroless Nickel: ASTM B733 Covers Ni-P Coatings

Top Metal Surface Finishing Methods for 2026

Electroplating and electroless nickel both add protective metal layers, but they work differently. Electroplating uses electric current to deposit metal. Electroless nickel relies on a chemical reaction, which can coat complex shapes without an external current. ASTM B733 addresses autocatalytic nickel-phosphorus coatings on metallic substrates. It sets requirements for coating types and service classes. Check the applicable edition and purchase specification before choosing a coating.

Geometry matters. Electroless nickel can reach recesses and internal passages more evenly, but uniformity is not automatic. Solution circulation, surface preparation, and fixture design all affect the deposit. A poorly cleaned bore can still become a weak point. That detail gets missed.

Specify the required thickness, phosphorus content, and inspection approach with the part’s operating conditions in mind. For example, a shaft exposed to wear may need different properties than a component facing a corrosive environment. Heat treatment can change hardness and corrosion performance, so confirm that any post-treatment suits both the component and the coating requirements. ASTM B733 is a useful reference, not a substitute for verifying the finished part. Real parts complicate this. It is worth checking.

Choose Anodizing, Conversion Coating, or Powder Coating for Metal Parts

Choosing between anodizing, conversion coating, and powder coating starts with the metal, its working environment, and the part’s geometry. A finish that performs well on an indoor bracket may fail on a marine-facing assembly. Check wear, moisture, appearance, and dimensional limits before selecting a process.

Anodizing is commonly used on aluminum. It builds an oxide layer from the metal itself, helping resist corrosion and surface wear without adding a thick film. It suits machined housings and components with tight fits, though edges and deep recesses may finish differently. Color can vary with alloy and processing. Test representative parts.

Conversion coating creates a thin chemical layer, often to improve corrosion resistance or paint adhesion. It can suit stamped parts and assemblies where minimal dimensional change matters. The result depends on the substrate and coating chemistry, so confirm compatibility with the specific metal and any later paint system. Thin does not mean indestructible.

Powder coating forms a thicker, cured film and offers a broad range of colors and textures. It works well for visible panels, frames, and equipment exposed to handling. Masking holes and threads matters; buildup can interfere with assembly. The curing heat also deserves attention, especially for heat-sensitive components.

I would not choose by appearance alone. Compare sample parts after realistic exposure, because one overlooked edge or contact point can change the outcome.

Classify Corrosion Exposure with ISO 9223’s Six C1–CX Categories

Top Metal Surface Finishing Methods for 2026

ISO 9223 classifies atmospheric corrosion into six categories: C1, C2, C3, C4, C5, and CX. The scale runs from very low to extreme corrosivity. It helps engineers describe exposure before choosing a metal finish, but it does not predict a coating’s exact service life.

C1 often describes clean, dry indoor spaces.

C2 may fit rural settings with limited pollution.

C3 covers many urban or mildly coastal environments, while C4 indicates more aggressive industrial or coastal exposure.

C5 represents very high corrosivity. CX is used for extreme conditions, such as severe marine exposure.

These are useful guides, not universal labels.

ISO 9223 assessments can use first-year corrosion rates for reference metals, including carbon steel, zinc, copper, and aluminum. Environmental factors such as chloride deposition, sulfur dioxide, and time of wetness can also inform classification.

A salt-laden breeze striking a sheltered loading bay may create a different risk from the wider region. Details matter. I have seen broad location labels hide such differences, and that is worth questioning.

Confirm the actual exposure before selecting a finish, especially near spray, standing water, or frequent condensation.

Conclusion

Metal Surface Finishing begins with preparing steel to the required cleanliness level. For demanding applications, abrasive blasting to ISO 8501-1 Sa 2½ can create a clean, consistent foundation before a finish is applied. Blasting, grinding, and polishing each produce different surface textures, so the method should be selected according to the required roughness, appearance, and function of the part.

The finishing process can then be matched to the material and its service environment. Electroplating and electroless nickel provide distinct coating options, with ASTM B733 addressing electroless nickel-phosphorus coatings. Anodizing, conversion coatings, and powder coatings offer alternatives for different metal parts and performance needs. Assess corrosion exposure using ISO 9223’s C1–CX categories, then use ISO 12944 durability bands—7, 15, and 25 years—as planning guides for coating life. Together, these choices help balance surface quality, corrosion protection, and expected maintenance.
Copyright 2025 Fluidra S.A. | Created by BCM Marketing Agencia Privacy Policy Legal note | Cookie policy |

Technical cookies are strictly necessary for our website to work and you can navigate through it. These types of cookies are those that, for example, allow us to identify you, give you access to certain restricted parts of the page if necessary, or remember different options or services already selected by you, such as your privacy preferences. Therefore, they are activated by default, your authorization not being necessary in this regard. Through the configuration of your browser, you can block or alert the presence of this type of cookies, although such blocking will affect the proper functioning of the different functionalities of our website.


The analysis cookies allow us to study the navigation of the users of our website in general (for example, which sections of the page are the most visited, which services are used most and if they work correctly, etc.). From the statistical information on navigation on our website, we can improve both the operation of the page itself and the different services it offers. Therefore, these cookies do not have an advertising purpose, but only serve to make our website work better, adapting to our users in general. By activating them you will contribute to this continuous improvement. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Functionality cookies allow us to remember your preferences, to personalize certain characteristics and general options of our website, every time you access it (for example, the language in which the information is presented to you, the sections marked as favorites, your browser type, etc.) Therefore, this type of cookies does not have an advertising purpose, but by activating them you will improve the functionality of the website (for example, adapting to your type of browser) and the customization of it based on your preferences (for example, by presenting the information in the language that you have chosen in previous occasions), which will contribute to the ease, usability and comfort of our page during your navigation. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Advertising cookies allow us to manage the advertising spaces included in our website based on criteria such as the content shown or the frequency in which the ads are displayed. For example, if you have been shown the same ad several times on our website, and you have not shown a personal interest by clicking on it, it will not appear again. In summary, by activating this type of cookies, the advertising shown on our website will be more useful and diverse, and less repetitive. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Behavioral advertising cookies allow us to obtain information based on the observation of your browsing habits and behaviors on the web, in order to show you advertising content that best suits your personal tastes and interests. To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.
To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.

SAVE

We use our own and third-party cookies to ensure the proper functioning of the website and to analyse our services, improve your experience on our website and show you advertisements related to your interests according to profiling based on your browsing habits (e.g. websites visited). You can accept all cookies by clicking "ACCEPT" or set or reject them by clicking here. If you would like to know more about the use of cookies, please see our COOKIE POLICY.


ACCEPT ALL
Reject no essentials