How to Choose the Right Die Cutting Machine?
FLUID HANDLING EXPERTS

Blog, all our news

How to Choose the Right Die Cutting Machine?

Choosing the right Die Cutting Machine can shape your production speed, material quality, and long-term operating costs. The decision should begin with your actual workflow, not a supplier’s most impressive specification. Consider the materials you process, such as paperboard, adhesive labels, foam, leather, or thin plastic. Each material responds differently to pressure, blade design, feeding methods, and machine speed. A machine that cuts cleanly through cardboard may damage delicate film or leave rough edges on thicker sheets.

Look closely at daily production details. How many pieces must be completed each hour? What size range will you need? Will operators change tools frequently? Experienced production teams often test samples before purchasing, checking edge quality, registration accuracy, noise, waste, and setup time. This practical step can reveal problems that brochures hide. It is easy to focus on maximum speed. That can be a mistake. A slower machine with stable feeding and simple adjustments may deliver better output over a full working day. Maintenance access also matters. Ask about blade replacement, spare parts, technical training, and service response times. Reliable support protects your investment when production schedules become demanding. However, no machine fits every workshop perfectly. Your first estimate may be incomplete. Review real orders, operator feedback, and future product plans before making a final choice. With clear requirements and careful testing, you can select equipment that supports consistent quality, safer operation, and sustainable business growth.

How to Choose the Right Die Cutting Machine?

Define Your Die Cutting Requirements and Material Specifications

How to Choose the Right Die Cutting Machine?

Define Your Die Cutting Requirements and Material Specifications

Start with the product, not the machine. Record the material type, thickness, sheet size, and required shape. Include foam, rubber, film, paper, or layered materials. Each behaves differently under pressure. A soft foam may compress before cutting. A rigid laminate may crack around narrow corners.

Measure the smallest feature carefully. Note hole diameters, edge tolerances, and spacing between cuts. Then estimate daily output, setup frequency, and acceptable waste. A machine for occasional prototypes may need flexibility more than speed. High-volume work demands stable pressure, repeatable positioning, and quick tool changes. Keep a physical sample nearby. Numbers alone can hide problems.

I once selected equipment based mainly on maximum cutting force. That assumption was wrong. The material stretched, and the finished parts varied by nearly one millimeter. Test the actual material with the intended die style and cutting pattern. Check whether adhesive liners separate cleanly. Examine the cut edge under normal lighting. It should not show tearing, compression, or unfinished corners. Leave room for trial adjustments. Real production conditions are rarely as neat as drawings.

Compare Die Cutting Machine Types and Operating Methods

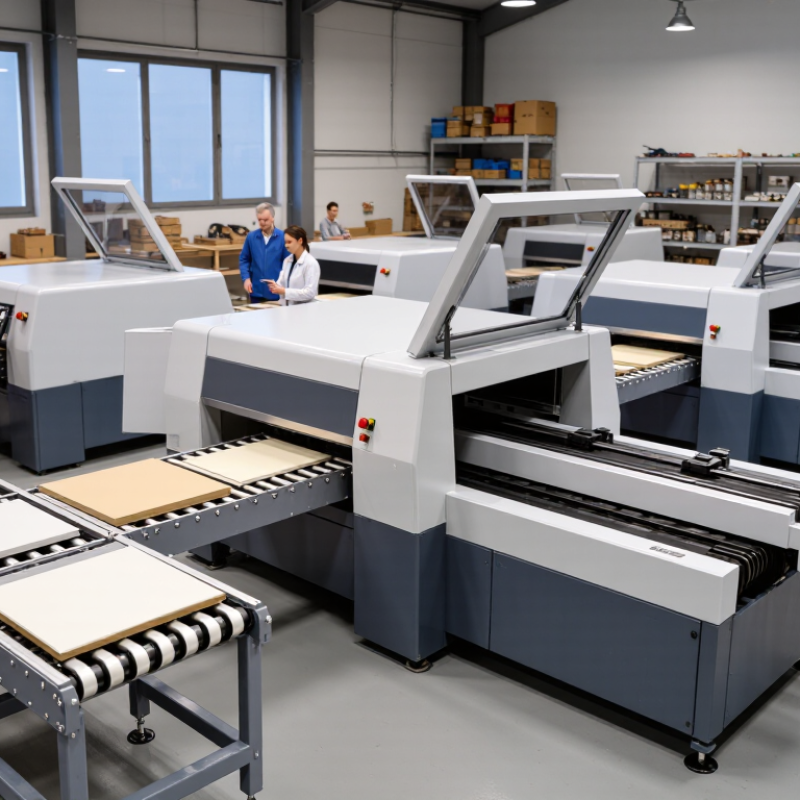
Choosing the right die cutting machine starts with comparing machine types and operating methods. A flatbed die cutter uses a fixed cutting form and pressing motion. It suits short runs, thick materials, and frequent design changes.

A rotary die cutter uses a cylindrical tool and continuous feeding. It performs better on long production runs and consistent materials.

The operating method affects both speed and control. Manual machines require direct feeding and pressure adjustment. They cost less, but output depends heavily on operator skill.

Semi-automatic machines reduce feeding work and improve repeatability.

Fully automatic systems manage feeding, cutting, waste removal, and stacking with limited intervention. They usually need more floor space and careful setup.

Speed can hide defects.

Material testing should happen before production. Check board thickness, surface coating, grain direction, and required tolerance.

A practical trial should inspect cut edges, registration, waste separation, and tool wear.

Rotary systems may create cleaner results at high volume, while flatbed systems offer easier adjustments for changing layouts.

Laser cutting can handle complex prototypes, but heat may discolor sensitive materials.

In real workshops, the fastest machine is not always the most productive.

I have seen operators choose high-speed equipment, then lose hours correcting feeding errors. A slower machine may be safer for delicate stock.

Record setup time, hourly output, maintenance needs, and operator training requirements. Leave room for mistakes; real materials rarely behave perfectly.

Evaluate Machine Capacity, Precision, Speed, and Automation

Choosing the right die cutting machine starts with actual production demands, not impressive brochure numbers. Measure material thickness, sheet size, repeat length, and daily volume. A machine rated for 500,000 cuts may struggle with dense board or long runs. Capacity must include usable pressure, feeding stability, and setup space. In my experience, slightly larger capacity reduces stress during seasonal peaks. Yet oversized equipment can waste energy and floor space. That trade-off deserves an honest review.

Precision protects every downstream process. Check cutting tolerance, registration control, waste removal, and tool alignment. Ask for sample runs using your own substrate, adhesive, and artwork. A clean edge on paper may not remain clean on laminated film. Measure real output, not only advertised strokes per minute. Faster cycling can create more rejects when feeding becomes unstable. Slow down briefly. Consistency usually matters more than maximum speed. Record defect rates across several hours, not one impressive demonstration.

Automation should remove repetitive handling without making operators helpless. Look for automatic feeding, sensor-based registration, quick changeover, production monitoring, and fault alerts. These features can shorten setup and improve traceability. However, complicated controls may require training and maintenance. I have seen teams choose advanced systems, then underuse half the functions. Review operator skills, service access, spare parts, and software support before buying. Leave room for improvement. Your first capacity estimate may be wrong, especially when new materials or custom jobs arrive.

Check Tooling, Maintenance, Safety, and Workspace Requirements

How to Choose the Right Die Cutting Machine?

Choosing a die cutting machine starts with the material, not the machine’s advertised speed. Start with the material. Test its thickness, hardness, surface finish, and expected cutting volume. A machine suitable for thin labels may struggle with dense rubber or layered insulation. During production trials, check tooling access, die alignment, and changeover time. Measure twice. A poorly matched die can create uneven edges, excessive waste, and costly delays.

Maintenance requirements deserve equal attention. Ask how operators will inspect blades, clean debris, lubricate moving parts, and verify pressure settings. Choose a design with accessible service points and clear maintenance instructions. Record inspection dates and replace worn tooling before defects become routine. I have seen teams focus on output speed while ignoring small alignment changes. That decision looked efficient at first, but it increased rework later.

Safety and workspace planning should happen before installation. Confirm guarding, emergency stops, safe loading procedures, and operator visibility. Follow the equipment manual and applicable workplace safety requirements. Keep enough room around the machine for maintenance, material handling, and emergency movement. Space matters. Consider noise, ventilation, lighting, floor strength, and nearby electrical connections. A compact machine may still create awkward traffic patterns. Leave room for pallets, tool storage, and imperfect human movement, because real workshops rarely stay perfectly organized.

How to Choose the Right Die Cutting Machine? — Check Tooling, Maintenance, Safety, and Workspace Requirements
Machine Type Best-Suited Materials and Jobs Typical Material Thickness Tooling Requirements Typical Production Profile Maintenance Requirements Safety Requirements Workspace Requirements Key Selection Consideration
Manual or Hand-Operated Flatbed Die Cutter Paper, board, thin foam, leather, gaskets, labels, prototypes, and short-run packaging. Commonly handles thin sheet materials up to approximately 3–6 mm, depending on machine capacity and material hardness. Steel-rule dies or custom cutting forms. Die height and cutting pressure must match the machine specification. Low-volume production and sampling. Suitable when frequent job changes and low initial investment are more important than speed. Clean the bed and platen regularly; inspect hinges, guides, pressure plates, and cutting surfaces; lubricate moving points according to the equipment manual. Use guards where provided, keep hands outside the cutting area, and use a documented safe operating procedure. Never bypass interlocks. Requires a stable, level workbench or floor position, adequate lighting, storage for dies, and clear access around the operating area. Choose this type when flexibility, prototypes, and small batches outweigh labor cost and automated feeding speed.
Hydraulic or Pneumatic Flatbed Die Cutter Corrugated board, foam, rubber, insulation, gaskets, textiles, composites, and formed packaging components. Often suitable for materials from thin sheets up to several millimeters, subject to press force, die height, and material compression. Steel-rule dies, solid cutting plates, stripping tools, and sometimes punching or creasing attachments. Medium-volume production with consistent pressure and repeatable cutting. Loading and unloading may be manual or semi-automatic. Inspect hydraulic hoses, pneumatic lines, filters, seals, pressure gauges, and cylinders. Remove debris and verify pressure settings during scheduled service. Requires guarding, emergency stops, two-hand controls or equivalent safeguarding, lockout/tagout procedures, and trained operators. Needs a rigid floor, sufficient headroom, service access, electrical power, and possibly compressed air or hydraulic service space. Check required cutting force, maximum die size, bed opening, stroke length, and whether the available utilities match the machine.
Automatic Flatbed Die Cutter Folding cartons, corrugated packaging, commercial print products, labels, and repeated sheet-fed work. Commonly processes paperboard and corrugated sheets; the allowable range depends on feeder, platen force, die design, and sheet format. Steel-rule cutting and creasing dies, stripping tools, make-ready sheets, and feeder or delivery adjustments. Medium- to high-volume production with automatic feeding, cutting, stripping, and delivery options. Requires scheduled cleaning, feeder calibration, lubrication, sensor inspection, die-board checks, and replacement of worn grippers or belts. Use fully enclosed guards, interlocked access doors, emergency stops, safe setup modes, and formal training for clearing jams. Requires a level industrial floor, material staging areas, die storage, operator access zones, and space for feeder and delivery sections. Prioritize sheet size, hourly output, setup time, registration accuracy, automation level, and availability of trained maintenance personnel.
Rotary Die Cutting Machine Labels, tapes, films, foils, flexible packaging, nonwovens, gaskets, and continuous web materials. Usually optimized for thin and flexible web materials, often from very thin films up to a few millimeters depending on the tooling and press design. Rotary magnetic-cylinder dies, solid rotary dies, anvil cylinders, slitting knives, and waste-removal tooling. High-speed, continuous production with efficient repeat processing and inline slitting, laminating, or rewinding. Monitor cylinder alignment, anvil wear, web tension, bearings, nip pressure, blades, sensors, and waste-removal systems. Guard rotating cylinders and nip points; use web-threading procedures, emergency stops, and lockout/tagout before entering the machine. Needs web-roll storage, unwind and rewind clearance, access for tooling changes, ventilation where adhesives are used, and a clean operating area. Choose this type when the material is supplied in a continuous web and speed, repeatability, and low waste are major priorities.
Digital Knife or Oscillating-Tool Cutter Prototypes, short-run packaging, textiles, leather, foam, corrugated board, composites, and materials requiring frequent design changes. Typically handles thin to medium-thickness materials; actual capacity depends on tool type, blade geometry, vacuum hold-down, and material density. Replaceable knives, oscillating blades, creasing wheels, perforation tools, and software-controlled tool heads. No dedicated steel-rule die is normally required. Low- to medium-volume production with fast design changes and minimal physical tooling lead time. Replace or sharpen blades, clean the cutting surface, inspect vacuum zones, calibrate the tool head, and maintain software and motion systems. Guard moving tool heads, use approved blades, control access during operation, and follow safe procedures for blade changes and vacuum systems. Requires a rigid table or conveyor, computer and network access, material loading space, extraction or dust control where needed, and stable power. Best for variable designs, prototypes, and jobs where avoiding die fabrication costs is more valuable than maximum throughput.
Laser Cutting Machine Paper, textiles, films, wood-based sheets, acrylic, selected plastics, and other materials approved by the equipment manufacturer. Thickness varies widely with laser power, material type, optical setup, and required edge quality; thin sheet processing is generally the most efficient. No physical cutting die. Requires lenses, mirrors or fiber-delivery components, focus settings, extraction filters, and suitable cutting parameters. Flexible prototyping and short- to medium-run production with digital pattern changes and no conventional die storage. Clean optics, inspect extraction filters, verify cooling systems, maintain air assist, check alignment, and remove cutting residue. Requires an enclosed Class 1 system or equivalent engineered guarding, fume extraction, fire protection, approved materials, and laser-specific training. Needs dedicated ventilation, non-combustible surroundings, stable power, cooling clearance where applicable, and controlled access to the work zone. Confirm material compatibility, edge discoloration tolerance, fume characteristics, required extraction capacity, and fire-risk controls before purchase.

Selection note: Actual capacity, force, speed, thickness, and utility requirements vary by machine design, tooling, material hardness, sheet format, and production method. Always verify the manufacturer’s technical documentation and conduct a sample test with the intended material before final selection.

Balance Purchase Cost, Operating Expenses, and Long-Term Value

How to Choose the Right Die Cutting Machine?

Balance Purchase Cost, Operating Expenses, and Long-Term Value

The lowest purchase price is rarely the lowest production cost. Evaluate the machine against your material, sheet size, cutting pressure, and expected volume. A unit designed for light cartons may struggle with thicker board, causing slower cycles and inconsistent edges. Request a practical test using your actual materials. Inspect registration, crease quality, noise, and setup time.

Operating expenses deserve equal attention. Measure power consumption, tooling costs, lubrication needs, and routine maintenance. Ask how quickly common parts can be replaced and whether operators need specialized training. A machine that saves ten minutes during setup can recover its extra cost over thousands of jobs. Small delays become expensive.

Long-term value is harder to calculate. Estimate annual output, expected downtime, service access, and the useful life of major components. Keep a written cost model with realistic production figures, not optimistic forecasts. No forecast is perfect. That matters. A machine may appear efficient during a demonstration but perform differently in a crowded workshop with changing operators. I would also leave room for mistakes, rushed setups, and future material changes. The right choice balances today’s budget with tomorrow’s workload, while protecting quality and operator confidence.

Copyright 2025 Fluidra S.A. | Created by BCM Marketing Agencia Privacy Policy Legal note | Cookie policy |

Technical cookies are strictly necessary for our website to work and you can navigate through it. These types of cookies are those that, for example, allow us to identify you, give you access to certain restricted parts of the page if necessary, or remember different options or services already selected by you, such as your privacy preferences. Therefore, they are activated by default, your authorization not being necessary in this regard. Through the configuration of your browser, you can block or alert the presence of this type of cookies, although such blocking will affect the proper functioning of the different functionalities of our website.


The analysis cookies allow us to study the navigation of the users of our website in general (for example, which sections of the page are the most visited, which services are used most and if they work correctly, etc.). From the statistical information on navigation on our website, we can improve both the operation of the page itself and the different services it offers. Therefore, these cookies do not have an advertising purpose, but only serve to make our website work better, adapting to our users in general. By activating them you will contribute to this continuous improvement. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Functionality cookies allow us to remember your preferences, to personalize certain characteristics and general options of our website, every time you access it (for example, the language in which the information is presented to you, the sections marked as favorites, your browser type, etc.) Therefore, this type of cookies does not have an advertising purpose, but by activating them you will improve the functionality of the website (for example, adapting to your type of browser) and the customization of it based on your preferences (for example, by presenting the information in the language that you have chosen in previous occasions), which will contribute to the ease, usability and comfort of our page during your navigation. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Advertising cookies allow us to manage the advertising spaces included in our website based on criteria such as the content shown or the frequency in which the ads are displayed. For example, if you have been shown the same ad several times on our website, and you have not shown a personal interest by clicking on it, it will not appear again. In summary, by activating this type of cookies, the advertising shown on our website will be more useful and diverse, and less repetitive. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Behavioral advertising cookies allow us to obtain information based on the observation of your browsing habits and behaviors on the web, in order to show you advertising content that best suits your personal tastes and interests. To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.
To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.

SAVE

We use our own and third-party cookies to ensure the proper functioning of the website and to analyse our services, improve your experience on our website and show you advertisements related to your interests according to profiling based on your browsing habits (e.g. websites visited). You can accept all cookies by clicking "ACCEPT" or set or reject them by clicking here. If you would like to know more about the use of cookies, please see our COOKIE POLICY.


ACCEPT ALL
Reject no essentials