How to Choose a Microwave Oven Baffle Die in 2026?
FLUID HANDLING EXPERTS

Blog, all our news

How to Choose a Microwave Oven Baffle Die in 2026?

Choosing a Microwave Oven Baffle Die in 2026 requires more than comparing catalog prices. The die must form thin, heat-resistant metal accurately, repeatedly, and with minimal burrs. Small errors can distort airflow openings, weaken mounting points, or create noisy vibration during operation.

David Chen, a senior sheet-metal tooling engineer with over 20 years of stamping experience, offers a practical warning: “A reliable die is measured by stable production, not by its first successful sample.” That principle matters when evaluating die steel, punch clearance, guiding accuracy, press compatibility, and expected service life. A polished trial part may hide early wear. Look deeper.

The best selection begins with the baffle’s material and thickness. Stainless steel, aluminized steel, and coated sheet may require different clearances and surface treatments. Check the required hole pattern, bend sequence, strip layout, and feeding direction. Ask whether the supplier has produced similar microwave components. Request inspection records, sample parts, and maintenance guidance.

Do not ignore the press. Its tonnage, shut height, stroke, and automation system must match the die design. Even an excellent die can perform poorly on unsuitable equipment. A cheaper quotation may look attractive. It may also conceal weaker inserts, limited testing, or expensive replacement work.

This guide examines those decisions for 2026. It also questions common assumptions. Maximum speed is not always the best target. Longer die life may matter more. Reliable evidence should guide the final choice.
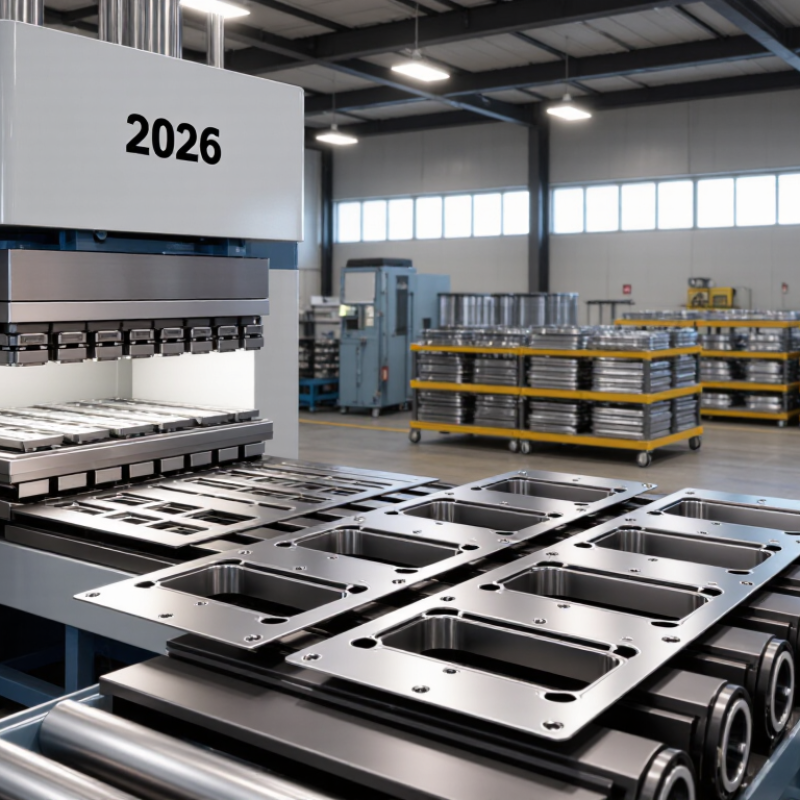
How to Choose a Microwave Oven Baffle Die in 2026?

What Is a Microwave Oven Baffle Die and What Does It Produce?

A microwave oven baffle die is a precision tool that shapes thin metal into the oven’s airflow or heat-distribution baffle. It produces formed plates, louvers, slots, mounting holes, and controlled bends in one repeatable process. In convection models, the baffle helps guide hot air around the cavity. In other designs, it supports airflow management near the heating system.

The die usually works with coated steel, stainless steel, or aluminum sheet. Its punch and forming sections must match the material’s thickness and springback. A small error can create sharp edges, poor airflow, or difficult assembly. According to Fortune Business Insights, the global microwave oven market was valued at about USD 10.8 billion in 2023, showing the scale behind this small tooling component. The report also expects continued market growth through 2032.

Tool selection should reflect production volume and baffle geometry. A progressive die suits high-volume parts with several operations. A compound die may be better for simpler blanks and lower tooling budgets. Industry 4.0 manufacturing reports from Deloitte emphasize process monitoring and reduced defect rates through connected equipment. That matters here. Still, digital simulation cannot replace a physical trial completely. I have seen a clean drawing produce a difficult part after forming. Material variation, burr control, and ventilation tests deserve careful review before final approval.
How Microwave Oven Baffle Dies Work in the Manufacturing Process

How to Choose a Microwave Oven Baffle Die in 2026?

How Microwave Oven Baffle Dies Work in the Manufacturing Process

A microwave oven baffle die converts flat sheet metal into a precise shielding or airflow component. The process usually includes blanking, piercing, bending, and final forming. A progressive die can complete several operations during one press stroke. This reduces handling, but it increases alignment risks. The die must match the material grade, thickness, press tonnage, and required production volume. World Steel Association’s World Steel in Figures 2024 reported 1,888.2 million tonnes of crude steel production in 2023. That scale also means material variation cannot be ignored. Even a small thickness change can affect springback and edge accuracy.

During production, sensors monitor strip feeding, punch position, and die pressure.

Operators then inspect hole diameter, flatness, burr height, and formed angles. ISO 9001 certification data from the ISO Survey 2023 shows more than 1.2 million certificates worldwide, reflecting the growing importance of documented quality control. Still, paperwork cannot replace practical testing. A prototype die may run well for one shift, then reveal cracking after repeated cycles. I would avoid choosing only by quoted price. Tool steel hardness, coating, replaceable inserts, cooling design, and maintenance access deserve equal attention.

Tips: Request a material trial before approval. Measure at least 30 sample parts. Check burrs under magnification. Record die wear after every production batch. A slower first trial often prevents expensive rework.

Which Materials and Design Features Affect Die Performance?

How to Choose a Microwave Oven Baffle Die in 2026?

Material selection directly affects baffle die life, accuracy, and maintenance. H13 hot-work tool steel commonly reaches about 44–52 HRC after heat treatment, according to ASM Handbook, Volume 14B. Carbide offers much higher hardness, often near 1,500–2,000 HV, but it is less forgiving during impact. A harder die is not automatically better. Thin stainless-steel baffles may need polished tool steel, while thicker blanks can justify carbide inserts in high-wear zones.

Thin stainless-steel baffles may need polished tool steel, while thicker blanks can justify carbide inserts in high-wear zones.

Design details matter just as much. Use generous corner radii to reduce cracking and avoid sharp transitions around the waveguide opening. Keep the punch guided closely, especially when clearance is narrow. The World Steel Association reported approximately 1.88 billion tonnes of global crude-steel production in 2024. That scale increases pressure for stable, repeatable forming, not merely fast tooling. ISO 4957 also separates tool-steel grades by intended service, reminding engineers to match steel properties with actual loading conditions.

Small errors become expensive.

In production trials, I would inspect burr height, springback, edge galling, and heat marks after every adjustment. Coatings can reduce friction, but surface preparation still controls adhesion. USGS Mineral Commodity Summaries 2025 notes continued dependence on globally traded chromium materials, so coating supply and cost deserve attention.

I would not select a die from hardness data alone. Material thickness, press tonnage, lubrication, and operator consistency can change the result. That part is often underestimated.

How to Match a Baffle Die With Microwave Oven Production Needs

How to Choose a Microwave Oven Baffle Die in 2026?

Microwave oven production is becoming more specification-driven. Grand View Research valued the global microwave oven market at approximately USD 11.5 billion in 2023. Its forecast also indicates continued growth through 2030. This demand makes die selection a production decision, not merely a tooling purchase. Match the baffle die to sheet thickness, material strength, cavity geometry, and monthly output. Thin galvanized steel may need a sharper forming radius. Stainless steel usually demands higher forming force and stronger wear protection. Check these details early.

Press capacity must exceed the calculated forming load, with practical safety margin. Review die clearance, guide-post accuracy, punch alignment, and ejection stability. A die that produces clean edges at 50 units per hour may struggle at 500. ISO 9001-based control practices can help document dimensional checks, material certificates, and first-article approval. Still, paper records do not replace a trial run. Real production sometimes exposes springback that simulations miss.

Tips: Ask for sample parts before approval. Measure flange height, corner radius, burr level, and flatness. Compare cycle time against the target volume. Leave room for maintenance access and quick insert replacement. An interchangeable-insert design may reduce downtime, but it can cost more initially. That trade-off deserves calculation. I would also test the die after several thousand strokes, because early results can look better than long-term performance. Industry reports provide direction, but your own press data should decide the final match.

How to Evaluate Quality, Maintenance, and Supplier Support in 2026

How to Choose a Microwave Oven Baffle Die in 2026?

A microwave oven baffle die must produce stable geometry, clean edges, and repeatable forming results. In practical audits, inspect the die surface under angled light. Small polishing marks can become visible defects after thousands of cycles. Check dimensional reports, steel certificates, heat-treatment records, and trial-run samples before approval. A perfect drawing is not enough.

Maintenance planning should begin before installation. Confirm access to wear components, lubrication points, spare inserts, and adjustment instructions. The U.S. Department of Energy’s microwave test procedures use controlled performance conditions, reminding engineers that small dimensional changes can affect final appliance results. Keep inspection records for burr height, alignment, and forming pressure. They reveal trends earlier than sudden failures.

Supplier support deserves equal attention. The ISO Survey 2023 recorded more than 1.26 million ISO 9001 certificates worldwide, but certification alone cannot prove die-making competence. Ask for response-time targets, remote troubleshooting procedures, and documented corrective actions. A supplier should explain how it measures tool life, not merely promise durability. I have seen attractive quotations hide weak after-sales support. That risk remains easy to underestimate. Select partners who provide measurable data, realistic maintenance intervals, and honest feedback when the original design needs revision.

How to Choose a Microwave Oven Baffle Die in 2026? — How to Evaluate Quality, Maintenance, and Supplier Support in 2026
Evaluation Dimension Recommended Requirement How to Verify 2026 Selection Benchmark Maintenance Implication Suggested Weight
Application Compatibility The die should match the baffle geometry, sheet thickness, material grade, forming direction, and required production volume. Compare the approved drawing, material specification, press capacity, shut height, and die envelope with the actual production equipment. Mandatory pass Correct compatibility reduces misalignment, excessive wear, and unplanned die modification. 15%
Die Material and Heat Treatment Use a tool-steel grade suitable for the forming load and expected production quantity, with documented hardness and heat-treatment records. Review material certificates, hardness test results, heat-treatment records, and dimensional stability after treatment. Documented and traceable Stable heat treatment helps reduce chipping, deformation, galling, and premature edge wear. 15%
Dimensional Accuracy Critical forming surfaces, locating features, and mounting interfaces should conform to the approved engineering drawing and tolerance scheme. Request a coordinate-measuring-machine report or equivalent inspection report for critical dimensions. 100% inspection of critical features Accurate locating and forming surfaces reduce setup time and repeated trial adjustments. 15%
Surface Finish Forming surfaces should be smooth, free from burrs, sharp unintended edges, grinding burns, and visible tool marks that could damage the baffle. Perform visual inspection and, where specified, verify roughness using a calibrated surface-roughness instrument. No burrs or scoring on contact surfaces Better finish reduces friction, material pickup, scratches, and cleaning frequency. 10%
Forming Consistency The die should produce consistent baffle height, angle, radius, hole position, and seating features throughout the production run. Run a representative sample batch and measure first-off, mid-run, and end-of-run parts against the approved inspection plan. Stable results across the sample run Consistent forming reduces sorting, rework, and corrective die adjustments. 15%
Burr and Edge Control Cutting and forming edges should be designed to limit burr formation and prevent sharp edges that can interfere with assembly or handling. Inspect representative parts under suitable lighting and measure burr height where a limit is defined by the product specification. Within drawing or process limits Lower burr formation extends tool life and reduces deburring labor and contamination risk. 8%
Guide and Alignment System Guide posts, bushings, locating pins, stops, and mounting surfaces should provide repeatable alignment and adequate rigidity. Check guide clearance, parallelism, mounting-hole accuracy, and repeatability after die opening and closing. Repeatable alignment without binding Replaceable guide components simplify servicing and protect expensive die plates. 8%
Inspection and Documentation The delivery package should include drawings, material certificates, inspection results, spare-part information, and operating instructions. Use a document checklist before acceptance and confirm revision numbers against the approved design. Complete documentation package Clear records support troubleshooting, audits, repairs, and future die reproduction. 7%
Routine Cleaning Remove metal particles, lubricant residue, and debris from forming surfaces, guides, vents, and scrap paths at a frequency based on production conditions. Check the supplier's cleaning method and confirm that it does not damage coatings, edges, or precision surfaces. Defined cleaning procedure Regular cleaning prevents scratches, buildup, blocked clearances, and inconsistent forming. Included in maintenance plan
Lubrication and Wear Monitoring Lubrication points and approved lubricant types should be clearly identified; wear limits should be defined for guides, inserts, and forming edges. Review the maintenance manual and verify that wear inspection points are accessible without major disassembly. Documented intervals and limits Controlled lubrication reduces friction while avoiding excess residue on microwave components. Included in maintenance plan
Repairability and Spare Parts High-wear components should be replaceable, standardized where practical, and identified by part number or drawing reference. Ask for a spare-parts list, replacement instructions, and the recommended stock level for critical items. Replaceable wear components Repairable construction reduces downtime and avoids replacing the entire die after localized wear. 5%
Supplier Technical Support The supplier should provide installation guidance, trial-production support, troubleshooting assistance, and controlled design-change communication. Evaluate response procedures, technical escalation contacts, service scope, and availability of remote or on-site support. Written support process Fast technical feedback helps resolve forming defects before they become recurring production problems. 7%
Acceptance and Warranty Terms Acceptance criteria should define dimensional conformity, sample approval, correction responsibility, warranty coverage, and response time. Confirm that all requirements are written into the purchase and acceptance documents before manufacture. Clear, measurable, and written Defined terms simplify claims, corrective action, and responsibility for early-life failures. 5%
Copyright 2025 Fluidra S.A. | Created by BCM Marketing Agencia Privacy Policy Legal note | Cookie policy |

Technical cookies are strictly necessary for our website to work and you can navigate through it. These types of cookies are those that, for example, allow us to identify you, give you access to certain restricted parts of the page if necessary, or remember different options or services already selected by you, such as your privacy preferences. Therefore, they are activated by default, your authorization not being necessary in this regard. Through the configuration of your browser, you can block or alert the presence of this type of cookies, although such blocking will affect the proper functioning of the different functionalities of our website.


The analysis cookies allow us to study the navigation of the users of our website in general (for example, which sections of the page are the most visited, which services are used most and if they work correctly, etc.). From the statistical information on navigation on our website, we can improve both the operation of the page itself and the different services it offers. Therefore, these cookies do not have an advertising purpose, but only serve to make our website work better, adapting to our users in general. By activating them you will contribute to this continuous improvement. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Functionality cookies allow us to remember your preferences, to personalize certain characteristics and general options of our website, every time you access it (for example, the language in which the information is presented to you, the sections marked as favorites, your browser type, etc.) Therefore, this type of cookies does not have an advertising purpose, but by activating them you will improve the functionality of the website (for example, adapting to your type of browser) and the customization of it based on your preferences (for example, by presenting the information in the language that you have chosen in previous occasions), which will contribute to the ease, usability and comfort of our page during your navigation. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Advertising cookies allow us to manage the advertising spaces included in our website based on criteria such as the content shown or the frequency in which the ads are displayed. For example, if you have been shown the same ad several times on our website, and you have not shown a personal interest by clicking on it, it will not appear again. In summary, by activating this type of cookies, the advertising shown on our website will be more useful and diverse, and less repetitive. You can enable or disable these cookies by checking the corresponding box, being disabled by default.


Behavioral advertising cookies allow us to obtain information based on the observation of your browsing habits and behaviors on the web, in order to show you advertising content that best suits your personal tastes and interests. To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.
To understand it in a very simple way, we will give you a fictitious example: if your last searches on the web were related to suspense literature, we would show you advertising about suspense books. Therefore, activating this type of cookies, the advertising that we show you on our website will not be generic, but will be oriented to your searches, tastes and interests, therefore adjusting exclusively to you. You can enable or disable these cookies by checking the corresponding box, being disabled by default.

SAVE

We use our own and third-party cookies to ensure the proper functioning of the website and to analyse our services, improve your experience on our website and show you advertisements related to your interests according to profiling based on your browsing habits (e.g. websites visited). You can accept all cookies by clicking "ACCEPT" or set or reject them by clicking here. If you would like to know more about the use of cookies, please see our COOKIE POLICY.


ACCEPT ALL
Reject no essentials